
RE-AL ACUREA-Coated HSS-E reamers from Monaghan Tooling deliver carbide level performance at one-third the cost
Monaghan Tooling Group (MTG) now offers RE-AL’s ACUREA-coated HSS-E precision reamers, a Swiss-made line that matches solid carbide feed rates and meets or exceeds carbide surface speeds at about one-third the tool cost.
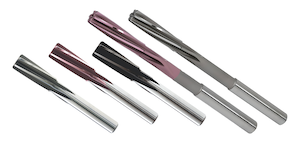 The two featured series, DIN 212 and DIN 8089, are ideal for aerospace, medical, and Swiss-type machining applications, where hole tolerance and finish are critical.
Tungsten prices have risen more than 200% in 2026, driven by tight supply and export controls, and carbide tool prices have followed. For many finishing operations, that increase buys no extra performance.
“With carbide prices climbing, many shops are paying a premium they don’t need on finishing operations,” said Kelly Burns, Vice President of Sales & Engineering at Monaghan Tooling Group. “ACUREA-coated HSS-E reamers run carbide-level speeds and feeds at about a third of the cost.”
What the Coating Delivers
ACUREA is a nanocomposite coating that gives HSS-E reamers carbide-class performance. The unique coating ensures the edge holds up to abrasive and hard materials (above 4,000 HV surface hardness), providing longer tool life between changes. Low friction stops the edge build-up, so finish and size stay consistent, producing cleaner bores with less scrap. The coating stays stable at the heat generated at two to three times uncoated HSS speeds, allowing carbide speeds without the carbide price. This nanocomposite coating allows the tooling to perform interrupted cuts and cross-drilled features without chipping, holding tight tolerances in challenging applications.
In RE-AL testing, a Ø6.15 mm DIN 8089 ACUREA reamer finished more than 400 holes in hardened D2 tool steel (1.2379) at 25 m/min (82 SFM) and 0.15 mm/rev. It held H6 tolerance and an N5 surface finish (Ra 0.4 µm / 16 µin) across the entire run, with minimal edge wear. (published cutting data available upon request).
Two Series Built for Precision Work
DIN 212 are straight-shank (h6) machine reamers with a left-hand 7–8° spiral and right-hand cut. They are available from 0.60 to 20.05 mm (.024” to .789”) in .01mm (.0004”) increments; these fine increments allow engineers to match a reamer to the exact bore instead of reworking the process to a standard size, making them ideal for small medical and aerospace features. Standard tolerance is 0/+0.003 mm under Ø2.65 mm and 0/+0.004 mm above (H7 and 0.005mm tolerances also available).
DIN 8089 are stub-length NC reamers built for precision holders and machining centers with limited tool space, which makes them a natural fit for Swiss-type lathes. Available from 03.76-13.20mm, with tolerance of 0/+0.004 mm. The shorter length improves rigidity and concentricity. Left-hand spiral for through holes, right-hand spiral (Ø3.76–13.20 mm) for blind holes.
Through-coolant is available on both series from Ø3 to 16 mm. Special geometries can be made to customer drawings.
https://monaghantooling.com/hss-e-solid-carbide-reaming/

INDUSTRIAL SUPPLY MAGAZINE
The September/October issue of Industrial Supply magazine features an in-depth cover story about Rotator Products. Plus, we're featuring articles by contributing writers Dr. Bharani Nagarathnam and Frank Hurtte, as well as interviews with numerous product and distribution industry experts.